Send inquiry
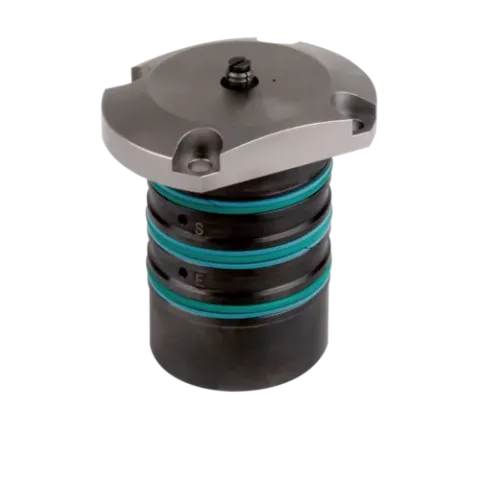
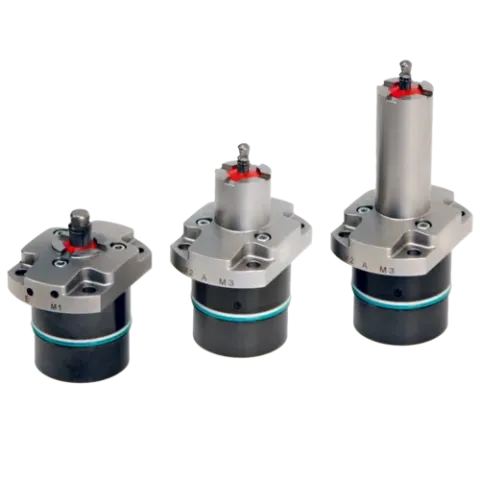
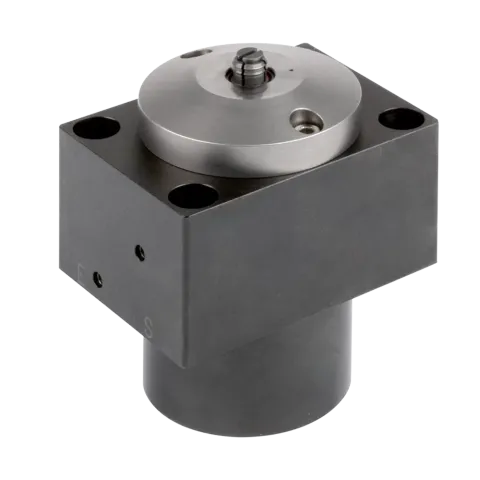
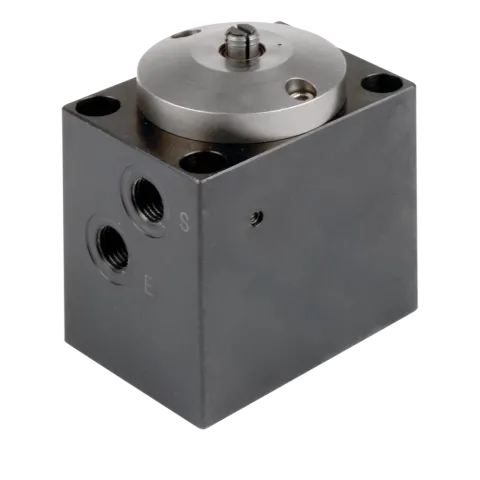
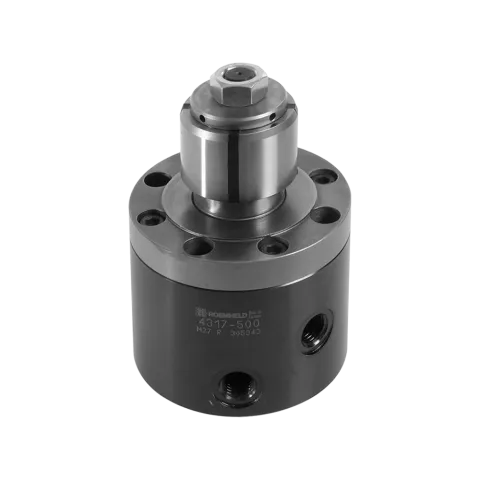
B 1.485 Bore clamp
The patented bore clamp is particularly suitable for positioning and clamping of workpieces with bore holes from diameter 6.6 to 13.8 mm in the support face. The workpiece is directly put onto the bore clamp, so that the remaining surfaces are free for machining on 5 sides. Due to its small and eccentric design the bore clamp can be placed very close to the workpiece contour. The variants with centring and compensation can compensate side loads. According to the load additional clamping forces can be necessary, since the axial clamping force is relatively small.
In the body of the bore clamp a double-acting hydraulic cylinder is mounted. By screwing in the clamping screw the piston actuates via a dowel pin a drive pin that is eccentrically arranged at the edge of the housing. The clamping ring is centred on a taper sleeve and hold by the head of the clamping screw. The clamping screw is secured by means of a thread coating against loosening. Penetration of liquids and swarf is avoided by the connection of positive air pressure protection.
Podobni produkti